Repair or Replace? Limits for Hydraulic Cylinder Rods and Barrels
Short answer: A scored cylinder rod can usually be polished and rechromed if the scoring is under about 0.1 mm deep. A barrel with wear under about 0.25 mm can be honed and fitted with oversize wear bands. Bent rods, deeper gouges, or rods ground below ISO f7/f8 size need a new rod turned from chrome bar.
Replacing complete hydraulic cylinders or bespoke actuator assemblies can lead to weeks of equipment downtime and steep costs. Learn how precision lathe machining, hard-chrome plating, and honing restore OEM tolerances faster and more economically.
ASAT Engineering Department
Machining & Fabrication Workshop
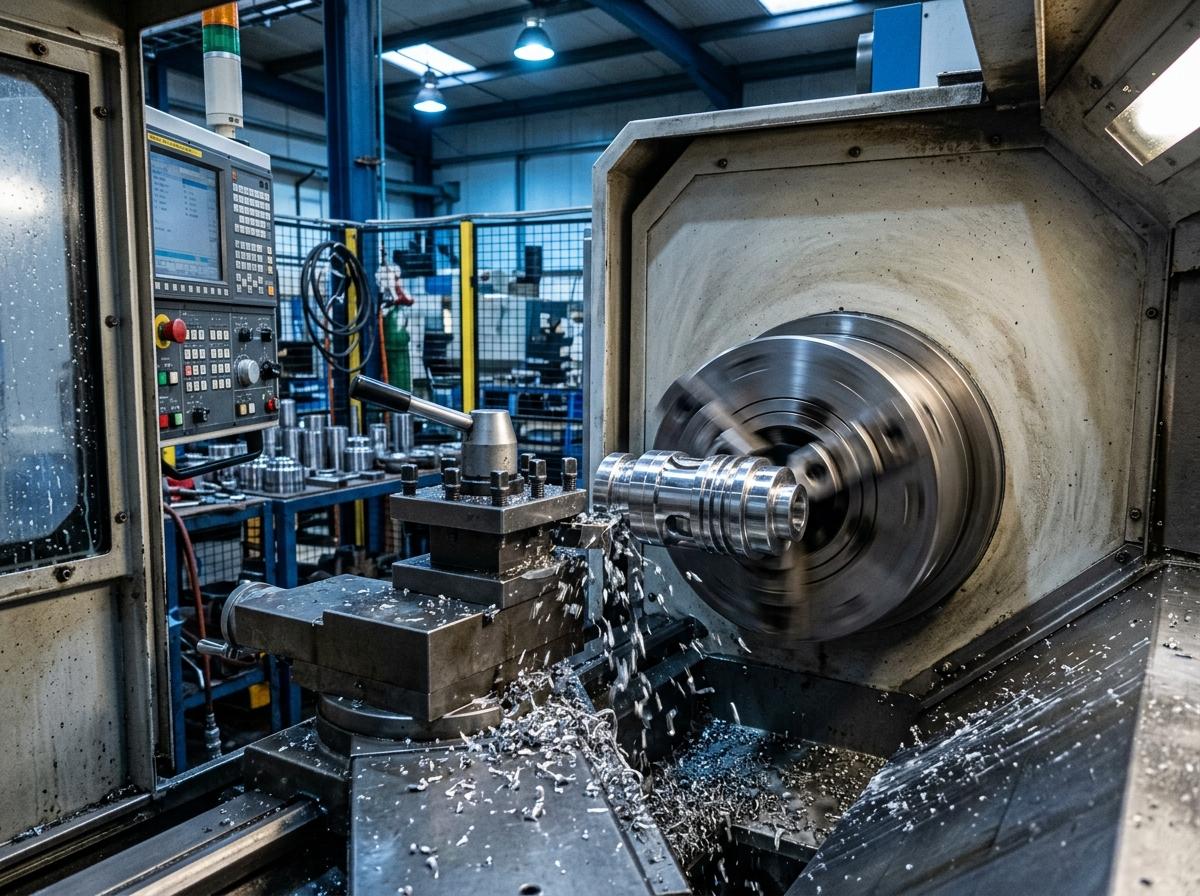
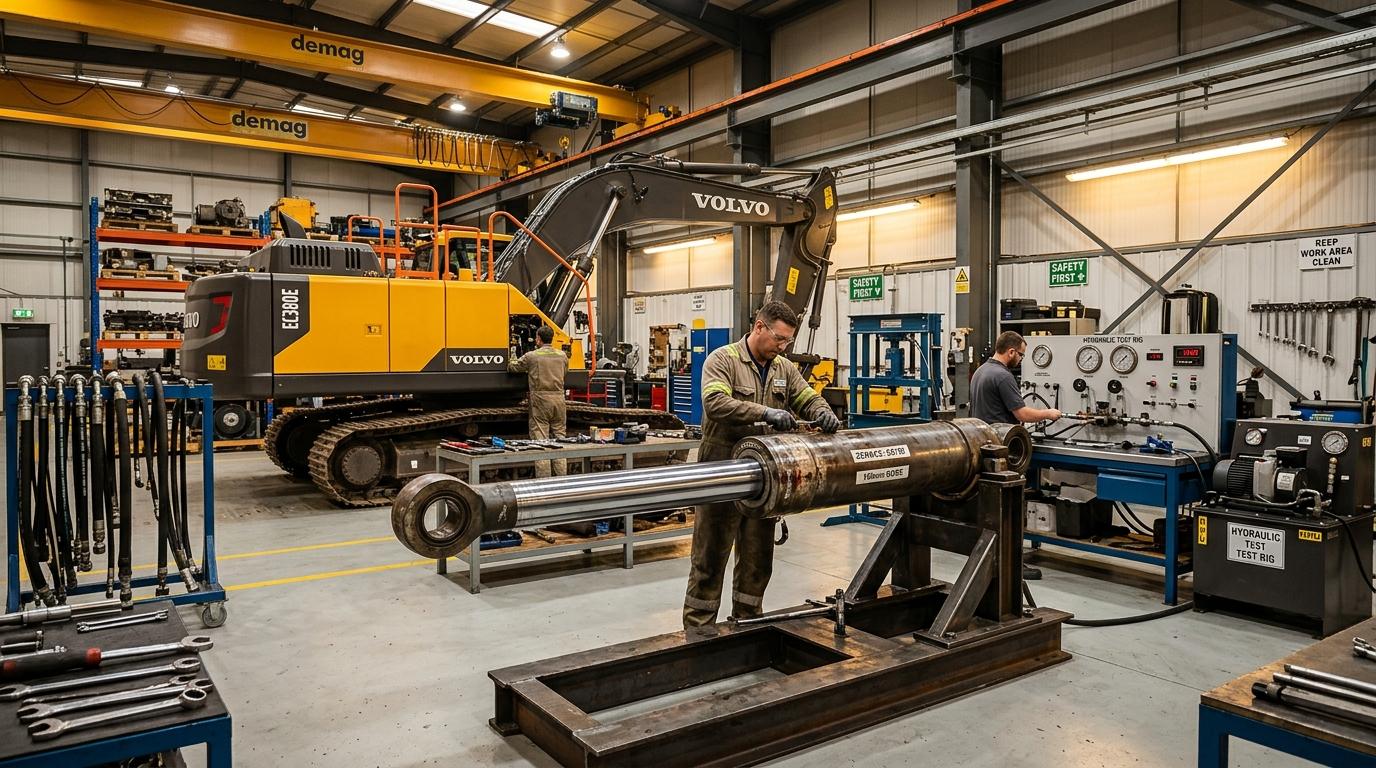
When large heavy machinery suffers hydraulic component damage on UAE construction, marine, or industrial sites, purchasing new OEM replacement assemblies often involves prohibitive lead times of several weeks and substantial capital expenditure. Precision workshop machining provides a verified engineering path to restore components to original dimensional tolerances and surface finishes.
The Recondition vs. Replace Evaluation
The decision to recondition versus replace relies on three rigorous engineering metrics: base material integrity, dimensional tolerance limits after material removal, and overall economic turnaround time.
- Scored Piston Rods: Minor scoring (<0.1mm) can be restored through precision micro-polishing and re-chroming. Deeper gouges or bent rods necessitate turning new rods from high-grade induction hardened chrome bar stock on our heavy-duty lathes.
- Barrel Ovality and Wear: Barrels with localized wear under 0.25mm can be honed to true cylindrical geometry, paired with oversize custom piston wear bands.
- Damaged End Eyes and Threading: Re-machining threads, line-boring pin eyes, and inserting hardened steel bushings restores structural integrity without barrel replacement.
Dimensional Limits for Rod Micro-Finishing
The dynamic rod seal depends on a tight radial interference and a specific surface finish roughness (typically Ra 0.2 to 0.4 μm). If grinding or polishing reduces the rod diameter below standard ISO f7/f8 tolerances, fluid weepage will occur regardless of how new the seal package is. In such cases, new chrome bar turning is the correct engineering procedure.
Cylinder Barrel Honing & Cross-Hatching
Honing is not merely about making the bore smooth. It creates an essential 30-to-45-degree cross-hatch pattern that retains microscopic lubricating oil films required to prevent polyurethane seal stick-slip and frictional degradation.
Custom Lathe Turning of Glands and Pistons
At ASAT Hydraulic Repairing, our machine shop utilizes industrial precision lathes to fabricate bespoke cylinder glands, pistons, manifolds, and bushings from certified high-tensile steels and phosphor bronzes, eliminating waiting periods for obsolete or discontinued equipment parts.
Frequently asked questions
How deep a scratch can a rod have?
- A scored rod can usually be polished and rechromed if the scoring is under about 0.1 mm deep. Deeper gouges, bends, or rods ground below size need a new rod.
What does honing do?
- Honing restores the round, straight bore of the barrel so new seals can seal properly. A barrel with wear under about 0.25 mm can usually be honed and fitted with oversize wear bands.
Is rechroming cheaper than a new rod?
- Usually, when the rod is straight and the scoring is shallow. A bent or deeply gouged rod is more economical to replace with a new rod machined from chrome bar.
Related Workshop Engineering Services
Hydraulic Cylinder Manufacturing, Repair & Maintenance
Reseal, honing, rechroming and new rods, tested to 350 bar.
Related Engineering Insights
Hydraulic Pump Cavitation: Causes, Warning Signs and How to Stop It
Understanding the physical mechanisms of vapor cavity implosion, intake line restrictions, and oil aeration that lead to premature axial piston pump destruction.
Why Hydraulic Cylinder Seals Fail in UAE Conditions, and How to Fix It
A practical guide to diagnosing extrusion damage, thermal hardening, abrasive scoring, and diesel effect across heavy equipment cylinder seals.
ISO 4406 Oil Cleanliness Codes Explained for UAE Hydraulic Systems
Why fluid contamination accounts for up to 80% of hydraulic component failures, and how to maintain strict ISO particulate target codes.
Have a Hydraulic Cylinder, Pump, or Valve Requiring Repair?
Consult directly with ASAT Hydraulic Repairing's senior technicians in the UAE. We provide comprehensive root-cause diagnostics, precise workshop teardowns, OEM-standard rebuilding, and certified pressure testing up to 350 bar.
Request a Service Quote
Share your machinery details for immediate technical evaluation.